Heavy Weldment Fabrication — Welded to Procedure, Machined After
We build weldments up to 4 tonnes in carbon, low-alloy and wear-resistant steel, and we finish-machine them in the same plant. Welding is done to qualified procedures with recorded parameters, not to whatever the welder is used to.
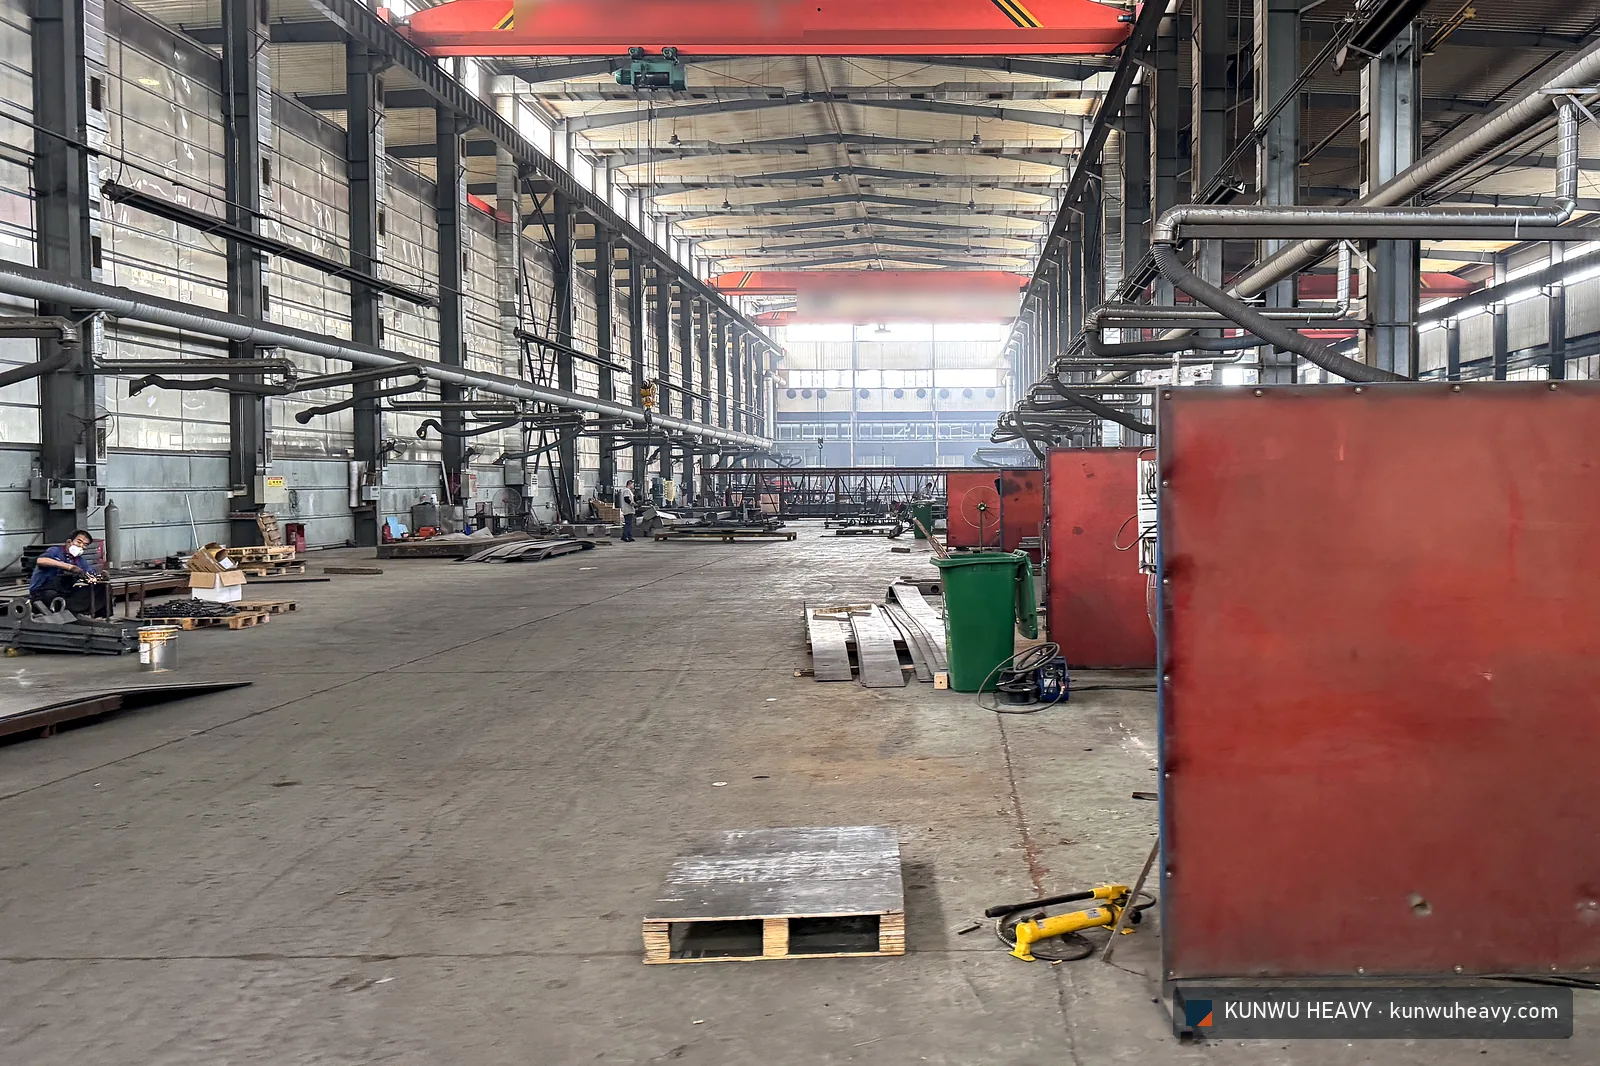
Capability
| Parameter | Value | Note |
|---|---|---|
| Max weldment size | 12000 × 4000 × 3500 mm | — |
| Max piece weight | 4 t | Limited by crane capacity |
| Crane capacity | 5 t × 2 | Single-girder EOT |
| Processes | MIG/MAG (135/136), TIG (141), SMAW (111), SAW (121), robotic | ISO 4063 |
| Max plate thickness welded | 80 mm | Multi-pass MAG / SAW |
| Welder qualification | EN ISO 9606-1 | Certificates travel with the job |
| Welding procedures | Qualified WPS with PQRs | EN ISO 15614 |
| Weld quality level | ISO 5817 Level C | Level B where specified |
| Dimensional tolerances | ISO 13920 Class B | Tighter class on request |
| Stress relief | In-house furnace, thermal cycle charts supplied | — |
| NDT in-house | VT, UT, MT | Third-party inspection on request |
- Thermal cutting to ISO 9013 Range 2 as standard.
- Weldment dimensional tolerances to ISO 13920 Class B as standard, a tighter class on request.
- Weld quality to ISO 5817 Level C as standard, Level B where the drawing specifies it.
- Machined features to ISO 2768-m unless the drawing states otherwise.
- Surface preparation to ISO 8501-1 Sa 2½, coating systems to ISO 12944 up to C4.
Distortion control
On a large weldment, distortion is a scheduling problem before it is a welding problem. We sequence the welds so the part pulls against itself, control interpass temperature on the alloy and wear grades, and stress-relieve before any machining.
Where a customer's design makes distortion unavoidable, we say so at quotation stage and propose a change — we would rather argue about it on a drawing than on a finished part.
Frequently asked
- Do you have welding procedure qualifications?
- Yes — qualified WPS with supporting PQRs to EN ISO 15614. We can send the relevant WPS with the quotation.
- Can you weld wear plate without losing hardness?
- Yes, with preheat and heat-input control appropriate to the grade and thickness. We do not weld across a wear face where the design allows the joint to be moved — and we will suggest that change if we see it.
- What weld quality level do you work to?
- ISO 5817 Level C as standard. Level B where the drawing specifies it, which changes the NDT scope and the price — tell us at enquiry stage.
- Do you do NDT in-house or subcontract it?
- Visual, ultrasonic and magnetic particle testing in-house. Radiography and third-party inspection by SGS, TÜV, BV or your own inspector are arranged on request.
Project pages are being prepared. If you want to see comparable work now, ask and we will send the relevant dimensional reports and photographs under NDA.
Send us the drawing
Acknowledgement within 4 working hours. Full quotation within 48 hours when the drawing package is complete.